+86 13638632902
 Jason@cleanroomequips.com


 MENU
Incomplete filtration, bad HVAC balancing, and poor design are reasons why most cleanrooms don't pass tests for compliance with the ISO standards. Even cleanrooms that seem to be finished may still not fully comply with tests for particle count, pressure differentials or time required to build up the cleanroom class.
It's rare that only one test failure is the cause. It's mostly due to several failures of the design, construction, commissioning, and operational functions. The best cleanroom designs already include all test procedures at the earliest design stage.
The High Cost of Cleanroom Non-Compliance
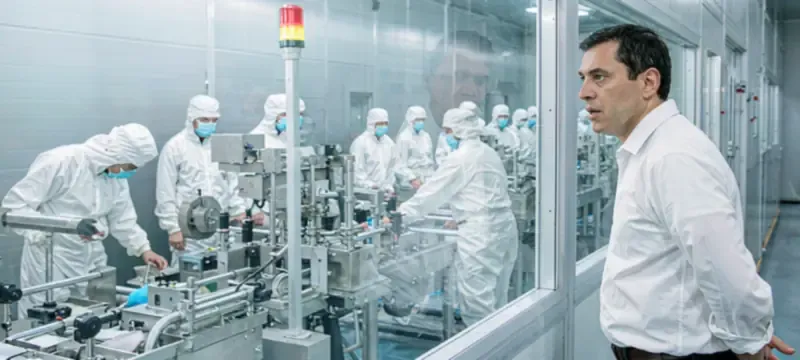
A cleanroom iso 14644 failure is more than a just a build failure. It brings production stops, failure of customer audit’s acceptance standards, job loss, and loss of profit due to the need for repairs.
Poor cleanroom HVAC systems are often invisible, and undiagnosed until final testing. By that time, corrective work often involves access to the ceiling, the removal of filters, the modification of ducts, and the reprogramming of the entire control system, and all of this must be done under a compressed schedule.
Risk profiles differ between industries, but regulatory compliance and audit failures result in patient safety concerns, costly product recalls, and compliance issues.
| Certification Stage | Condition | Failure Rate | Common Causes |
|---|---|---|---|
| As-Built | Empty room, no equipment | ~10% | Filter leaks, poor seal integrity, duct leakage |
| At-Rest | Equipment installed, no personnel | ~20% | Pressure imbalance, equipment heat plume disturbance |
| Operational | Full production, staff on site | ~70% | Personnel particle shedding, material flow disruption, dynamic pressure drift |
| As-Built — Empty Room |
|---|
| Failure rate: ~10% |
| Causes: filter leaks, poor seals, duct leakage |
| At-Rest — Equipment Only |
| Failure rate: ~20% |
| Causes: pressure imbalance, heat plumes |
| Operational — Full Production |
| Failure rate: ~70% |
| Causes: personnel shedding, material flow, pressure drift |
Mistake 1 — Improper HVAC Airflow Pathing and Pressure Balancing
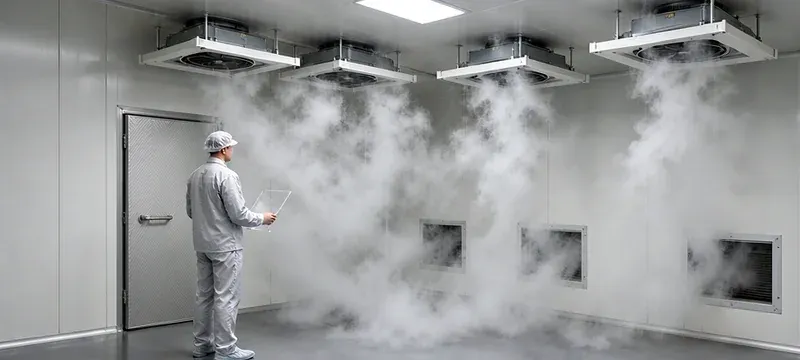
Unstable pressure gradients in combination with bad airflow patterning are the most frequent causes for a failure of cleanroom pressure differentials. Even if the correct volume of air is supplied, it will not be fully functional unless the air follows the intended path.
Common design errors in this category include:
- Supply and return airflow volumes are mismatched across zones
- Pressure cascades between adjacent rooms are incorrectly graded
- Personnel and material airlocks break pressure relationships
- Return vent placement creates localized airflow short-circuiting
- Duct static pressure calculations underestimate system resistance
- Variable frequency drive range is too narrow for real load variation
- Door opening events cause rapid pressure loss and recovery lag
- Equipment heat loads are omitted from airflow and capacity calculations
ISO 14644 Key Design Benchmarks
- Pressure differential: 10–15 Pa between classification zones; ≥15 Pa from clean zone to unclassified space
- air change rate (ACH): iso 5: 120–180 ACH; ISO 6: 60–90 ACH; ISO 7: 30–60 ACH; iso 8: 10–20 ACH
- Recovery time: Class 5/6 cleanrooms should recover within 5–10 minutes after disturbance
Validation tests that expose these flaws include airflow velocity mapping, room differential pressure measurement, smoke visualization, air change rate verification and recovery time testing.
Figure 1: Airflow balancing and pressure differential testing in ISO classified cleanroom
Mistake 2 — Inadequate Filtration and Filter Seal Integrity
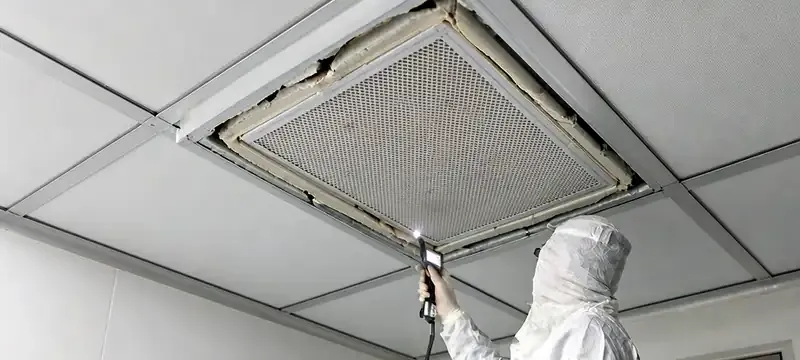
HEPA filters alone are insufficient to guarantee particle control. HEPA filter leakage test failure is among the most known reasons cleanrooms fail ISO tests, even with new filter media.
Seal and installation failures include:
- Filter efficiency grade mismatched to process risk level
- Uneven filter mounting frame surface
- Insufficient gasket compression around filter perimeter
- Gaps between filter bank frame and ceiling grid
- Inadequate sealing between adjacent ffu housings
- No re-test after filter replacement or maintenance
- No tracking of filter identity, installation date or pressure history
Filter Integrity Test Standard
- PAO / DOP leak test: Leakage rate exceeding 0.01% of upstream challenge concentration constitutes a failure
- Scan speed: Maximum 5 cm/s across filter surface and all perimeter seals
- Required frequency: After installation, after each filter change, and at scheduled re-certification
Leak paths contour the filter media. Particle counters may read acceptable levels at the ceiling level, but contamination enters through the gaps at the filter edge, corners of the frame, or ceiling penetrations.
Mistake 3 — Poor Material Selection and Surface Finish
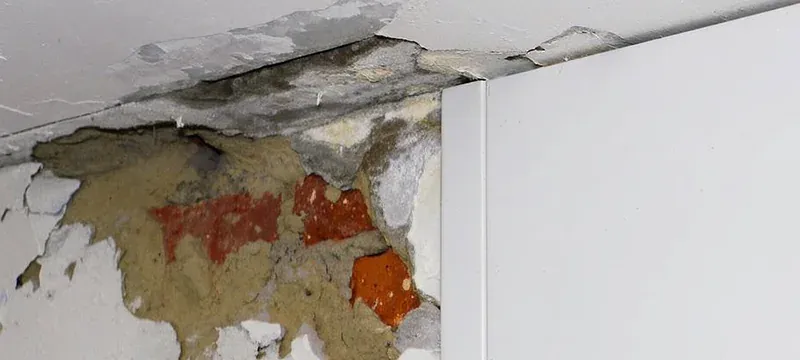
Mistakes in the selection of cleanroom wall panels and poor surface selection can negate the work done in optimal the design of an HVAC system. Surfaces can trap dirt and contaminants and shed particles that resist disinfection.
Common material and finish problems:
- Rough or porous wall surfaces that accumulate and release particles
- Sharp internal corners that create dead zones and resist cleaning
- Unsealed joints at wall-floor, wall-ceiling and wall-wall transitions
- Poor perimeter sealing around doors, viewports and pass-throughs
- Surface coatings degraded by routine disinfectants and cleaning agents
- Exposed fasteners, rivets and fixtures that trap contamination
- Ceiling grid systems with poor seal integrity and load deflection
The low bid contractors use construction silicone instead of using cleanroom sealants as a result of cost cutting measures, and use generic construction silicone. After control the VHP hydrogen peroxide sterilization cycle, the generic construction silicone surfaces crack, outgas VOCs, and shed micro-particles. So please always specify cleanroom-certified sealants.
Mistake 4 — Insufficient Monitoring and Control Systems
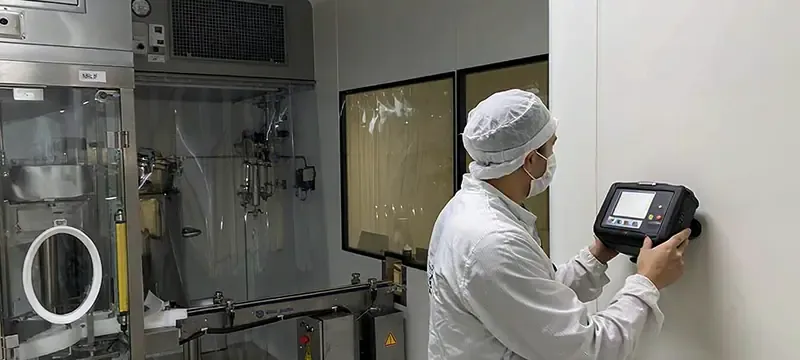
A cleanroom can pass a one-time acceptance test and drift out of cleanroom specifications during normal operations. Without regular and continuous monitoring of cleanroom pressure and environment, issues will stay hidden until a failure occurs.
Key parameters requiring continuous monitoring:
- Room differential pressure across each zone boundary
- Temperature and relative humidity setpoint control
- Airborne particle concentration at work height
- Fan operating state and airflow feedback
- Filter differential pressure across each stage
- Door position and interlock status
- Alarm logging, historical trending and audit trail export
The control system performance issues include poor sensor placement, lack proper calibration, incorrect alarm thresholds, poor integration of the BMS system, lack historical data, poor recovery from power loss, and lack training for the operating personnel.
Mistake 5 — Overlooking Personnel, Material and Process Flow
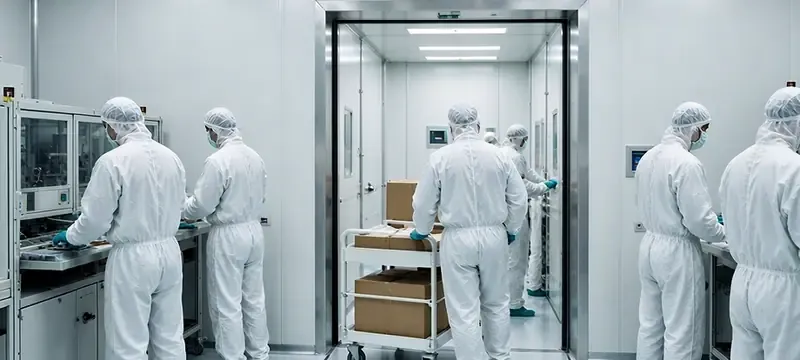
Smoke and material handling can bring in contamination faster than the air handling and pumping system can remove it; this can happen even if the HVAC system is perfectly designed.
Common operational design errors:
- Personnel entry and material entry share the same airlock
- Incomplete gowning procedure and staging sequence
- Insufficient buffer and airlock staging between classes
- Pass-through chambers that can be opened on both sides simultaneously
- Direct open passage between classification levels
- Waste stream routes cross raw material paths
- Insufficient operator training and behavior protocol
- Door interlock systems bypassed or out of service
Gaps in the system often appear only in dynamic operation. During daily operations, the system alters from the predictable and intended interactions of staff, components and waste. Static Certification tests performed at minimal occupancy may fail to capture these significant gaps.
Common Test Tools for Cleanroom Certification
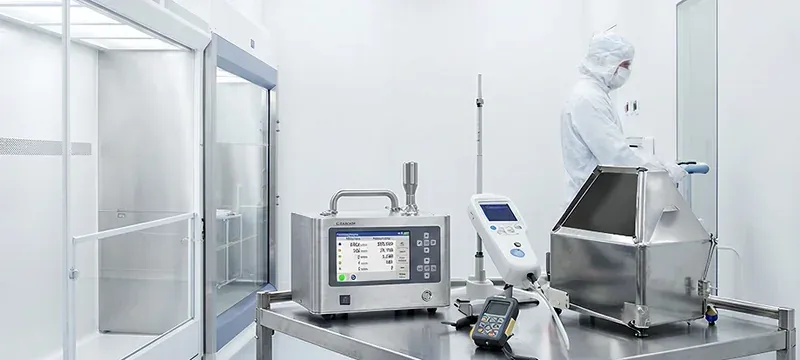
Certification technicians use standardized instruments to identify the root cause of failure. The most common tools include:
How to Diagnose Why a Cleanroom Failed ISO Testing
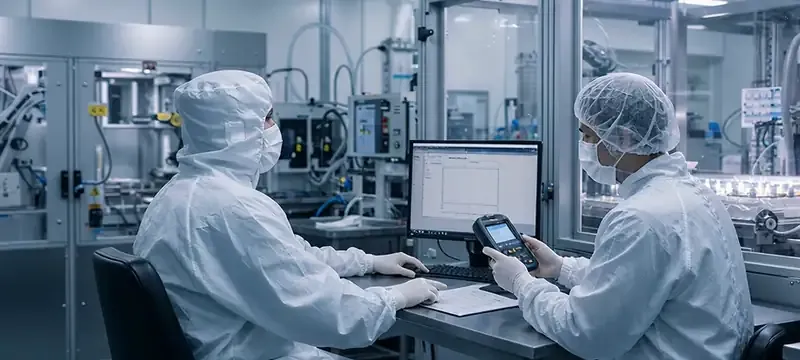
When investigating cleanroom failures of ISO Tests, a stepwise approach should be followed in the simplest to most complex, most invasive sequence.
Failure modes fall into four primary categories:
| Failure Symptom | Most Likely Root Causes |
|---|---|
| Particle concentration exceeds limit | HEPA filter leakage, poor airflow distribution, excessive personnel activity, surface contamination, insufficient recovery time |
| Pressure differential out of range | Airflow balance error, envelope leakage, slow control response, incorrect cascade design |
| Air velocity / air change rate too low | Undersized fan, excessive filter pressure drop, miscalculated duct loss, poor FFU layout |
| Recovery time too long | Insufficient supply air, poor source containment, inefficient return path, mismatched room volume |
| Particle Concentration High |
|---|
| HEPA filter leakage |
| Poor airflow distribution |
| Excessive personnel activity |
| Pressure Differential Off |
| Airflow balance error |
| Envelope leakage |
| Slow control response |
Cleanroom Air Change Rate Calculator
Estimate required air change rate and total supply airflow based on room dimensions and target ISO classification.
Recommended Air Change Rate: 0 – 0 ACH
Minimum Supply Airflow: 0 m³/h
Maximum Supply Airflow: 0 m³/h
Deiiang Case Study — Retrofitting a Cleanroom That Failed Certification
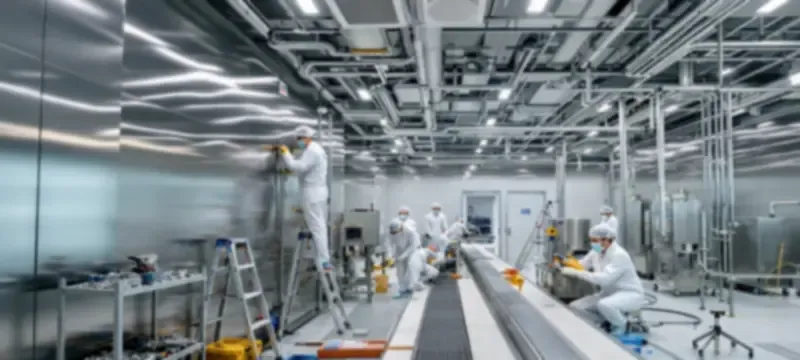
Project profile: ISO Class 7 Semiconductor Manufacturing Cleanroom, 2,200 m², with an FFU-based ceiling system. The facility failed the initial third-party certification and required a targeted retrofit with minimal impact to production.
Known issues before retrofit:
- Restricted ceiling height limiting duct modification options
- Existing ductwork could not be fully demolished
- Production line permitted limited shutdown window
- Pressure cascade between rooms was inconsistent
- Legacy BMS interface had limited integration capability
- High local humidity increased dehumidification load
Deiiang remediation scope:
- Recalculated zone airflow and pressure gradient balance
- Repositioned supply and return vent locations for improved sweep
- Resealed and leak-tested HEPA filter banks
- Added variable frequency fan control with trim response
- Installed differential pressure and RH/T sensor network
- Integrated monitoring platform with alarm and trending
- Phased commissioning and verification plan
- Revised personnel flow and material transfer procedures
Verified Project Improvement
Data source: Deiiang on-site commissioning report. Pressure stability improved from ±8.0 Pa to ±1.5 Pa across all classified zones.
Product design by Jason.peng, Deiiang™ cleanroom engineering team.
Integrated vs Fragmented Cleanroom Design
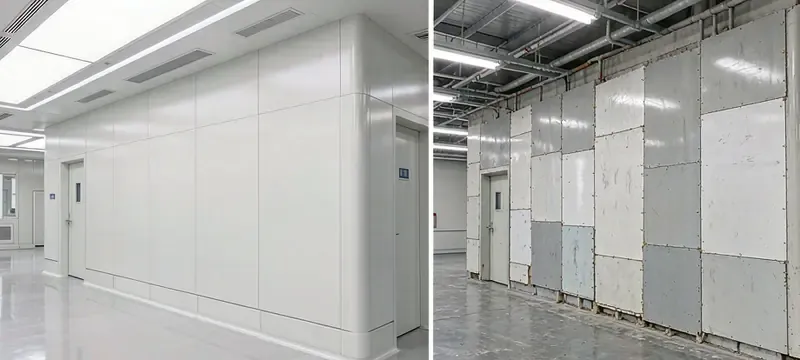
Certification risk increases significantly when HVAC, panels, controls, and filtration systems are provided by separate vendors with no accountable designer. An integrated approach connects all disciplines to the same performance model.
Integrated Engineering Approach
- HVAC, filtration and controls designed as one system
- Airflow and pressure relationships validated before testing
- Simpler troubleshooting and unified documentation
- Better alignment between construction and commissioning
- Single point of responsibility for certification performance
Fragmented Installation Approach
- HVAC, panels and controls use inconsistent assumptions
- Problems often discovered only during certification
- Higher risk of rework and schedule delays
- Responsibility for failed testing may be unclear
- Cross-vendor disputes slow corrective action
Pre-Certification Checklist for Cleanroom Owners
Use this checklist before formal ISO testing to identify gaps early and reduce the risk of failure.
Frequently Asked Questions
Why do cleanrooms fail ISO testing?
The primary causes of ISO test failures are ballasting airflow, instability of pressure differentials, HEPA leaks, seal and structural integrity failures, contamination and personnel control failures. The majority of these failures, 70%, are present when the cleanroom is operating at full capacity.
What are the most common cleanroom HVAC errors?
Some of the more common HVAC errors include the failure to account for duct pressure loss, improper return vent placement, fan undersizing, inadequate VFD range setting, improper placement of cascades, and improper sensor placement.
Can a cleanroom pass testing without a monitoring system?
cleanrooms are able to “pass” system acceptance tests, however without a monitoring system, the cleanroom will fall from an acceptable classification during normal operations. The pressure, filtration and humidity systems will not be operating within acceptable thresholds until the next classification test is performed.
How can Deiiang help with cleanroom certification?
Deiiang™ offers a full range of cleanroom design and HVAC and FFU systems, filters with leak testing, pressure and humidity control, combined with on-site commissioning, pre-certification repairs and testing support and documentation.